
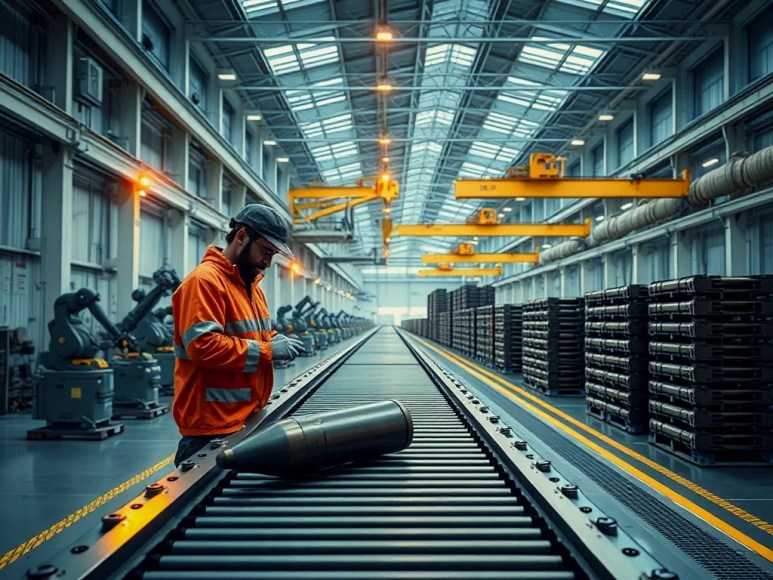
BAE Systems launches the UK’s first fully automated large-calibre ammunition plant in Glascoed
BAE Systems opened a new, largely robotic explosive-filling facility at its Glascoed site in Wales to scale 155 mm artillery shell production toward a target 16-fold increase over 2023 levels. The plant integrates industrial robots, automated material handling, and autonomous guided vehicles to minimize direct human exposure to energetic materials, speed duty cycles and raise operational safety. Commissioning and live trials remain under way, so full-rate serial production has not yet started.
How the facility’s automation changes production
The plant replaces manual handling steps with closed automated workflows. Melt-cast explosive is prepared within controlled environments, dispensed into shell bodies by robotic metering systems, and transferred between process cells by autonomous vehicles. Robots handle precision tasks such as nozzle positioning, in-line weighing and non-contact inspection, while environmental enclosures and machine interlocks reduce contamination and risk.
Step-by-step process flow implemented at Glascoed:
1. Controlled melt-cast preparation and filtration of energetic feedstock.
2. Automated transfer to metering stations inside sealed cells.
3. Robotic nozzle filling of 155 mm shell bodies with closed-loop weight feedback.
4. Automated cool-down and tempering under monitored conditions.
5. Robotic finishing, inspection (visual, dimensional, non-destructive) and transfer to assembly or storage.
Example benefits: continuous operation windows beyond standard human shift patterns, repeatable fill tolerances reducing ballistic variance, and faster, auditable traceability for batch quality control.
What “16× capacity” specifically means and current limits
BAE calculates the 16-fold figure against its 2023 throughput baseline; it denotes an expected long-term production ceiling rather than an immediate jump on day one. Practical constraints that will determine the realized rate include completion of commissioning, validated live-fire quality trials, supply of raw energetic materials, certified workforce for oversight, and regulatory approvals for full-scale deliveries.
Typical timeline dependencies:
– Commissioning and systems validation: robotics, sensors and safety interlocks undergo staged validation with inert media before energetic processing.
– Qualification firing: lots of representatives must pass ballistic and safety tests.
– Supply-chain ramp: consistent feedstock volumes and logistics must align with automated takt times.
– Regulatory and export controls: certifications and licenses can affect shipment cadence.
Why melt-cast suits automated large-calibre filling
Melt-cast filling deposits a viscous energetic composition into pre-formed shell bodies, then allows controlled solidification. This method suits automation because it uses metered liquid flows, predictable thermal cycles and sealed handling—properties compatible with robotic dosing and reduced human access. At Glascoed, melt-cast cells pair temperature-controlled kettles with precision metering pumps and automated cool-down racks to ensure consistent energetic density and minimize voids.
Operational example: a robotic metering loop measures fill mass within ± small gram tolerances, then initiates a programmed cool-down profile that avoids shrinkage defects—reducing rework and scrap rates compared with manual casting.
Safety architecture and risk mitigation in an automated energetic plant
Automated energetic plants prioritise layered controls. Glascoed’s architecture likely combines:
– Physical isolation: sealed process cells and blast-protective layouts.
– Process automation: PLC- and safety-PLC-driven interlocks with deterministic shutdown on anomalies.
– Robotics governance: certified SIL-rated controllers and force-limited end-effectors where human entry is occasionally required.
– Environmental monitoring: continuous temperature, pressure and gas detection with automatic venting and suppression.
– Traceability: digital batch records and machine logs to support root-cause analysis and regulatory audits.
These controls collectively shorten incident response times, lower worker exposure and increase consistency of safety-critical tasks such as heating control and fill verification.
Industrial and strategic impacts for the UK and European supply chains
Adding automated melt-cast capability in Glascoed strengthens the UK’s indigenous artillery shell production and reduces dependence on external suppliers for 155 mm ammunition—an item in higher demand across NATO and European forces since recent inventory drawdowns. The facility forms part of a £180 million UAE investment program intended to increase national resilience by expanding domestic capacity, modernizing processes and shortening lead times for wartime surge production.
Practical implications for customers and planners:
– Faster surge capacity: automated plants can scale operating hours and batch cadence to meet spikes in demand.
– Predictable quality: tighter tolerance control reduces out-of-spec shipments and rework burden on downstream assembly.
– Supply diversification: domestic output reduces transport dependencies and potential export-policy constraints.
Operational caveats: why opening does not equal full deliveries
Public opening marks a construction and commissioning milestone, not the start of full-volume deliveries. Glascoed still requires staged live trials, qualification firings and regulatory clearance. Manufacturing at declared capacity hinges on sustained raw-material supply chains, trained supervision personnel for automated systems, and validated quality performance across ballistic and safety regimes.
Real-world precedent: modern defense factories often open with automated lines active for inert materials and ramp to energetic production over months to ensure perfect alignment of process control and test outcomes.
Quotes and leadership view
BAE’s Digital Intelligence & Land Group head stated that combining Glascoed’s decades of munitions experience with modern automation will raise throughput and resilience. The comment emphasizes continuity of local expertise alongside technological upgrade rather than a wholesale replacement of skills.
What to watch next: metrics and milestones to verify the 16× claim
Stakeholders should monitor:
– Commissioning milestones: completion of live energetic trials and safety sign-off.
– Qualification lot results: ballistic testing, environmental aging and fragility metrics.
– Production cadence data: published annual output figures and batch-size disclosures.
– Supply-chain contracts: long-term feedstock agreements that enable sustained throughput.
– Export and regulatory filings: timelines for shipment approvals and customer deliveries.
Tracking these items will reveal whether the plant delivers the projected capacity uplift in practice.
Short example scenarios: realistic ramp profiles
Conservative ramp: 6–12 months of inert commissioning, followed by 6–12 months of energetic qualification, then phased capacity increases reaching 50% of target in year two and full capacity by year three, assuming steady feedstocks.
Aggressive ramp: parallelised commissioning and qualification achieve initial energetic batches within 4–6 months, reaching 75% of target by the end of year one if supply-chain and approvals alignment.
Conclusion: practical significance
The Glascoed facility represents a concrete step toward modernizing UK artillery shell production through automation and melt-cast techniques. The 16× figure indicates potential scale rather than an immediate outcome; Realization depends on commissioning, qualification, supply continuity and regulatory clearance. If Glascoed achieves its aims, it will provide faster, more consistent domestic supply of 155 mm ammunition to meet allied requirements.